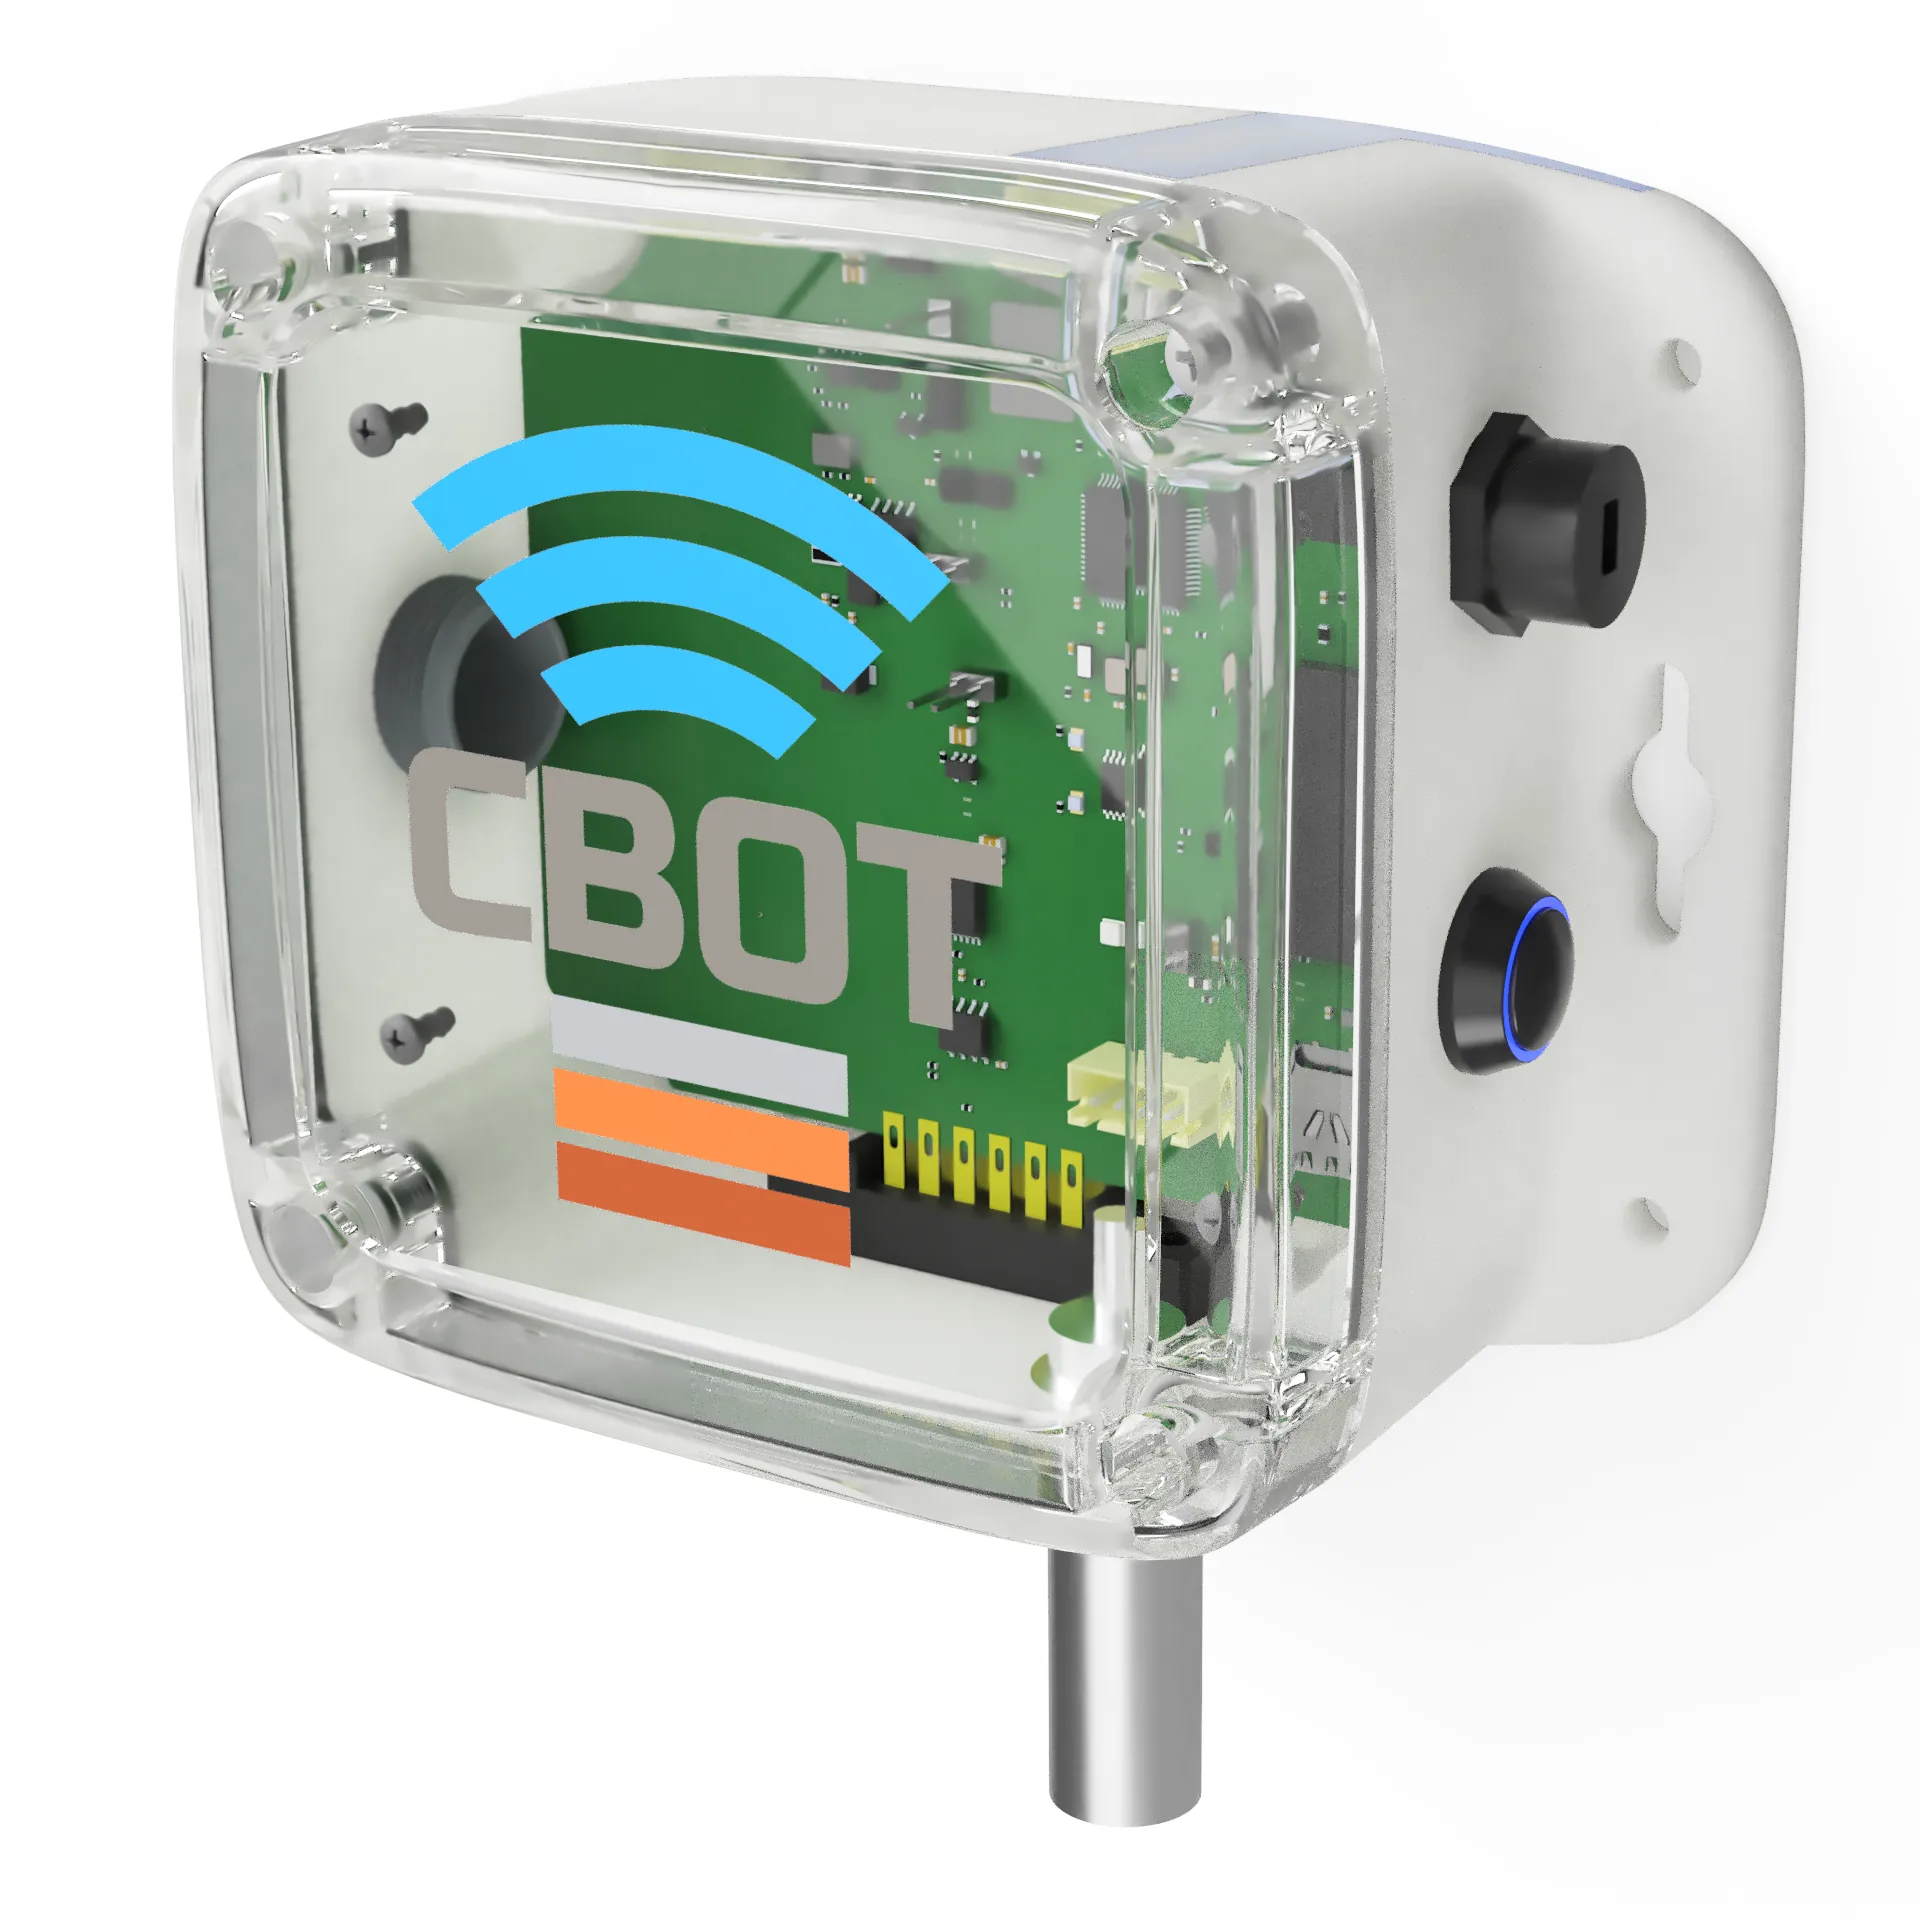
A render made before tooling has one job: to show the part the mould will actually produce. So before I light anything, I spend the first hour or so inside the CAD checking parting lines, draft, wall thickness, fasteners, the gasket and the gaps between the two halves. If those are wrong in the model, the image will be pretty and useless, and it'll be the picture everyone remembers when the first shots come off the tool looking different.
Most enclosure jobs reach me as a STEP file and a deadline. Here's what I open first.
Why a pre-tooling render is a different job
Marketing renders of a finished product are forgiving. The product exists, so there's a physical thing to match and somebody will tell me if the grey is too warm. Before tooling there's nothing to match. The render becomes the reference: investors see it, the sales deck is built around it, a crowdfunding page may promise it, and six months later a moulder delivers something with a visible split line across the front face and a 0.5 mm step where the lid meets the base.
Nobody lied. The model was simply cleaner than physics allows.
That's why I treat these jobs as half engineering review, half visualisation. I'm a mechanical engineer before I'm a visualiser, and on enclosure work that order matters more than anywhere else.
Parting line and draft: what the mould adds to your design
Every moulded half has a parting line, and it will be visible to some degree. In CAD it usually doesn't exist at all. So the first check is simple: where will the tool split, and does the model show it? If the split runs around the widest perimeter of the base, fine, I model a fine witness line there (around 0.05 to 0.1 mm deep, just enough to catch light). If it has to cross a cosmetic face, the client should hear that from me now, not from the toolmaker in week nine.
Draft is the second check. I run Fusion 360's draft analysis along the pull direction and look at the vertical walls. Smooth walls want at least 1 degree, and textured ones more, with roughly 1 extra degree for every 0.025 mm of texture depth as a starting rule. A 60 mm tall wall with 2 degrees of draft leans in by about 2 mm from bottom to top. That changes the silhouette. A box that looked crisp and square in the concept render now tapers, and in a three-quarter view you can see it.
Should the render show the taper? Yes. Always.
Walls, ribs and the sink marks nobody models
Next comes a section view through every screw boss and rib. I'm looking for thick spots: a 2.5 mm wall with a 2.5 mm rib behind it, or a boss merged into a corner. Those will sink on the outside face, and on a glossy black housing a sink mark reads from across the room.
I don't add fake sink marks to a render (that'd be strange), but I do two things. I flag the spots to the client with a screenshot, because fixing a rib ratio costs ten minutes in CAD and a lot more in steel. And I steer the finish. If the design can't lose the thick sections, a light texture on the outer face hides what gloss would advertise. Then I render the texture, not the gloss. The image and the eventual part agree.
Wall thickness matters for translucent parts too. A light pipe or a smoked lid in 1.5 mm polycarbonate transmits very differently from the 3 mm slab a concept modeller drew, so I set the real thickness before I touch the material.
Gaps, steps and fasteners
CAD assemblies are usually modelled line to line. Lid touches base, button touches bezel, zero gap. Real parts can't do that. A button needs roughly 0.2 to 0.3 mm of clearance all round or it sticks, a lid-to-base joint typically gets a deliberate 0.3 to 0.5 mm reveal so tolerance variation hides inside a shadow line, and a gasket needs a groove and something like 20 to 30% compression to seal.
These tiny numbers do most of the work in making a render look real. A zero-gap model renders like a single lump of plastic with lines drawn on it. Add a 0.3 mm reveal with a 0.2 mm edge radius and suddenly the light breaks along the joint, a thin shadow appears, and the thing looks manufactured.
Then fasteners. Where are the screws? I've lost count of the models where the two halves are held together by nothing at all. If there are four M3 screws going in from the bottom, the underside view needs four counterbores, and somebody needs to decide whether rubber feet cover them. If it's snap fits, there'll be a small slot or pry point somewhere. This is the list I run through on every housing:
- Screw positions, head type and whether they're visible from any planned camera.
- Cable exits, glands and connector cut-outs with the real connector in place.
- Vents, label recesses and the regulatory marking area.
- Gate location, if it's known, and ejector pin marks on any face a customer will see.
A sensor housing that changed after one screenshot
Last year a founder sent me the STEP for a sealed outdoor sensor enclosure (a base, a transparent lid, a gasket and a PCB) and asked for five images for a pitch deck. The lid in the model was flat, 2 mm thick, with a perfectly sharp outer edge and no draft anywhere. Lovely to look at.
I sent back one section screenshot with three arrows: no draft on a 45 mm wall, no groove for the gasket (it was floating in an interference), and screw bosses sitting directly against the outer wall. Their engineer fixed all three in about two days. The renders went out a little later than planned, and the housing in the deck had a slight taper, a visible seal line and four screws on top. Less sleek, honestly. But it was the product.
What goes into the image, and what stays out
People assume the honest version means showing every flaw. It doesn't. I leave out ejector marks on hidden faces, flow lines and minor gate vestige, the things a customer never notices on a decent part. I put in everything that changes shape, proportion or finish: draft, reveals, parting line position, real radii (a moulded outside edge is never truly sharp, and 0.3 to 0.5 mm is a sensible minimum), texture grade and the true colour of the resin as far as anyone knows it.
Resolution and render settings are the easy part by comparison. For enclosure stills I normally work at 4000 px on the long side, somewhere between 512 and 1,024 samples in Cycles with denoising, which lands at 6 to 15 minutes a frame on my machine depending on how much clear plastic is in shot. Transparent lids over a PCB are the slow ones.
One note on the PCB, since it comes up constantly. If the board is visible through a window, I need the real board export, or at least the real outline with the tall components. A generic green rectangle under a clear lid is the fastest way to make an engineer distrust the whole image.
What I'd actually do before paying for renders
Freeze the outside first. Not the whole design, just the exterior surfaces, the split and the fastening method. Then get a manufacturability pass on that geometry, from your moulder if you have one or from an engineer who's dealt with tooling, and only then commission images. Doing it the other way round means paying twice, once for the pretty version and once for the true one.
If the design isn't frozen and you need pictures anyway (fundraising rarely waits), say so. I'll build the scene so that a revised STEP drops in without redoing lights and materials, and I'll keep the cameras away from the areas most likely to move. That's a perfectly reasonable way to work. Pretending the concept is final is the mistake.
And ask whoever renders it one question: what did you change or flag in my model? If the answer is "nothing", either your CAD is unusually good or nobody looked.
I do both sides of this. The check comes from my work as a product development engineer, the images from 3D product rendering, and when the model needs fixing instead of flagging, that's a job for CAD design services. If you have an enclosure heading for tooling, send me the STEP and I'll tell you what I'd change before anyone lights it.